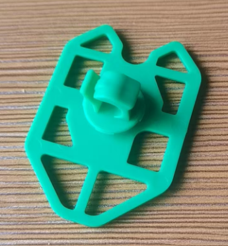
Multi-Cavity Mold Solution for Automotive Clips
Product Requirements:
Automotive clips with high production volume, thin wall thickness, and light weight. The part has certain demolding features, and the mold layout requirements are demanding.
Product Overview:
Material: POM. Surface finish: SPI-B1. Dimensions: 47 × 33 × 15 mm. Wall thickness: 1 mm. Mold cavitation: 1 × 24.
Mold Solution:
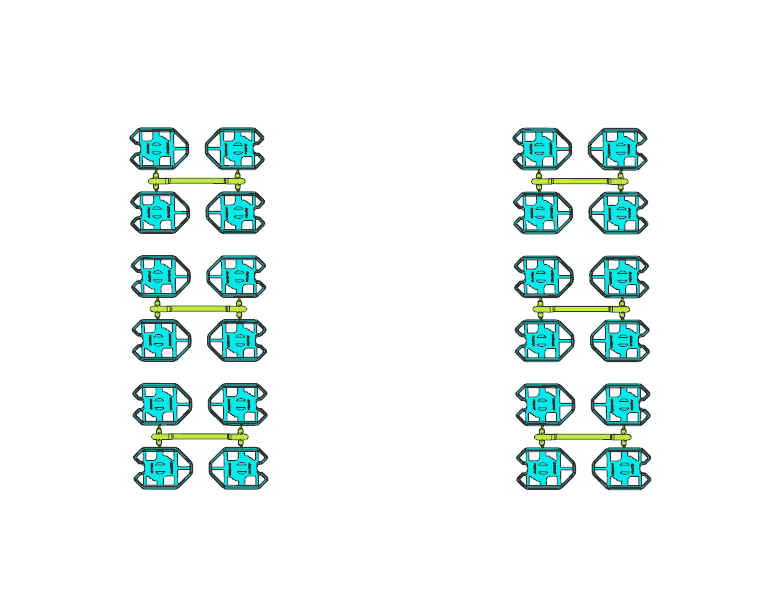
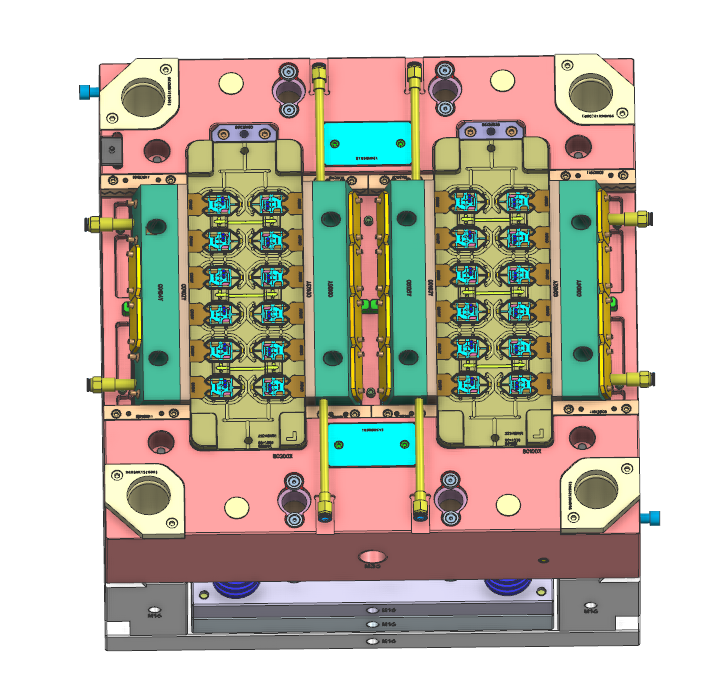
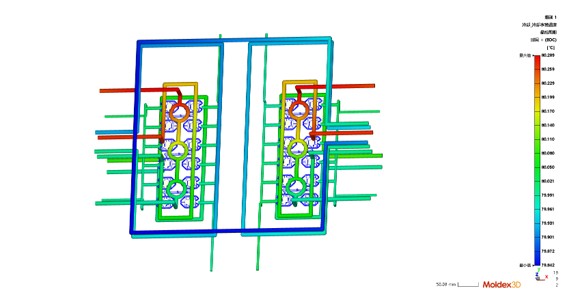
For this multi-cavity mold, the part layout was optimized to the extreme. An inverted mold structure combining slides and lifters was adopted, allowing the mold to run on a 200T injection molding machine. For the thin-walled parts, a hot runner plus cold runner sub-gate (tunnel gate) design was used, with one hot runner nozzle feeding four parts. Precise mold flow analysis verified the feasibility of the solution, greatly reducing mold cost. Because it is a multi-cavity mold, each group of parts was assigned its own dedicated cooling circuit, ensuring consistent mold temperature for every part and guaranteeing dimensional stability.
Result Feedback:
Every detail of the mold was well executed from design to manufacturing, achieving a truly high-quality mold. The mold achieved mass production readiness at T1, and the customer was very satisfied.